Size the Operating Modes Before You Size the Duct
Industrial exhaust systems are often sized too early, before the operating philosophy is fully defined. That is where apparently reasonable duct diameters can become difficult to balance later.
The design basis should state which hoods, tools, tanks, enclosures, or process connections operate simultaneously; whether branches are constant-volume, manually gated, or modulated; what minimum capture or control airflow each source requires; and what happens during startup, cleaning, maintenance, or upset conditions. A main duct serving six branches does not necessarily carry the arithmetic sum of all six design flows—but it must carry the correct coincident load for every credible operating mode.
Once branch airflow is established, the continuity relationship is straightforward: Q = V × A. For a round duct, A = πD² / 4. Experienced designers use that relationship to generate candidate diameters, then test those diameters against the rest of the system rather than treating the first answer as the specification.
Velocity Should Follow the Service, Not a Rule of Thumb
There is no single industrial-exhaust velocity that is correct for every PVC system. OSHA ventilation guidance distinguishes between general duct velocity and minimum transport velocity, and process-specific standards prescribe minimum velocities where solids must remain suspended. A corrosive vapor stream, an acid mist, a wet aerosol, and a particulate-laden exhaust do not present the same transport problem.
For vapor-only service, increasing velocity usually reduces diameter but raises velocity pressure and tends to increase fitting and straight-duct losses. For particulate or droplet service, reducing velocity may create deposition or carryover problems even if the pressure calculation looks attractive. Noise, available fan pressure, energy use, branch balance, duct availability, and process constraints all enter the tradeoff.
The useful question is therefore not “What velocity should PVC duct run at?” It is “What velocity range is defensible for this contaminant, operating mode, and system objective?” PVC is the duct material; it does not determine the aerodynamic design velocity by itself.
Compare Candidate Diameters Instead of Solving for One Number
Consider a branch that must move 5,000 CFM. Rather than selecting one assumed velocity and accepting the calculated diameter, compare practical sizes and see what each does to the system.
At 18 inches inside diameter, the average velocity is about 2,830 fpm. At 20 inches, it is about 2,290 fpm. At 22 inches, it falls to about 1,890 fpm. None of those values is automatically right or wrong. The 18-inch option may reduce space and material but increase velocity pressure and system resistance. The 22-inch option may reduce aerodynamic loss but require more room, larger fittings, different supports, and possibly custom fabrication. If the exhaust carries material that requires a minimum transport velocity, the larger diameter may be unacceptable regardless of its lower pressure loss.
| Candidate ID | Area | Velocity @ 5,000 CFM | Design Implication |
|---|---|---|---|
| 18 in | 1.77 ft² | ~2,830 fpm | Compact; higher velocity pressure and loss tendency |
| 20 in | 2.18 ft² | ~2,290 fpm | Mid-range; verify standard/fabricated availability and total pressure |
| 22 in | 2.64 ft² | ~1,890 fpm | Lower velocity; larger footprint/fittings; check transport requirement |
That is the level at which industrial PVC duct sizing becomes a specification decision: diameter, velocity, pressure loss, available components, structural construction, and installed geometry have to be evaluated together.
The Controlling Path Sets the Fan Duty
The controlling path is the route from a source through the duct system to the fan and discharge that requires the greatest total pressure capability under the design operating condition. It is not always the physically longest branch.
A shorter run can govern if it includes a high-loss hood entry, several elbows, an abrupt transition, a control device, or a scrubber connection. Conversely, a long straight run may be relatively benign if its diameter and velocity keep friction loss low. The pressure calculation should therefore be built segment by segment using the actual airflow, selected diameter, straight-duct friction, fitting losses, equipment losses, and inlet/outlet conditions for each operating mode.
This is also where fan selection and duct sizing become inseparable. A fan curve evaluated without the installed system resistance is incomplete, and a duct layout evaluated without the fan operating point is equally incomplete. The specified system should deliver the required source airflow at the expected resistance—not merely at a catalog free-air condition.
Fitting Geometry Can Matter More Than Another Few Feet of Straight Duct
Compact industrial exhaust systems often concentrate a large share of their pressure loss in elbows, branches, transitions, dampers, and equipment connections. That becomes especially important near the fan, where poor inlet conditions can create system effect and reduce installed fan performance compared with ideal test conditions.
A tight elbow directly at a fan inlet, an abrupt reducer, or a poorly proportioned branch can impose a penalty that is not obvious from duct diameter alone. AMCA guidance treats these inlet and outlet disturbances as system-effect issues because swirl, nonuniform velocity profiles, and turbulence can change how the fan actually performs.
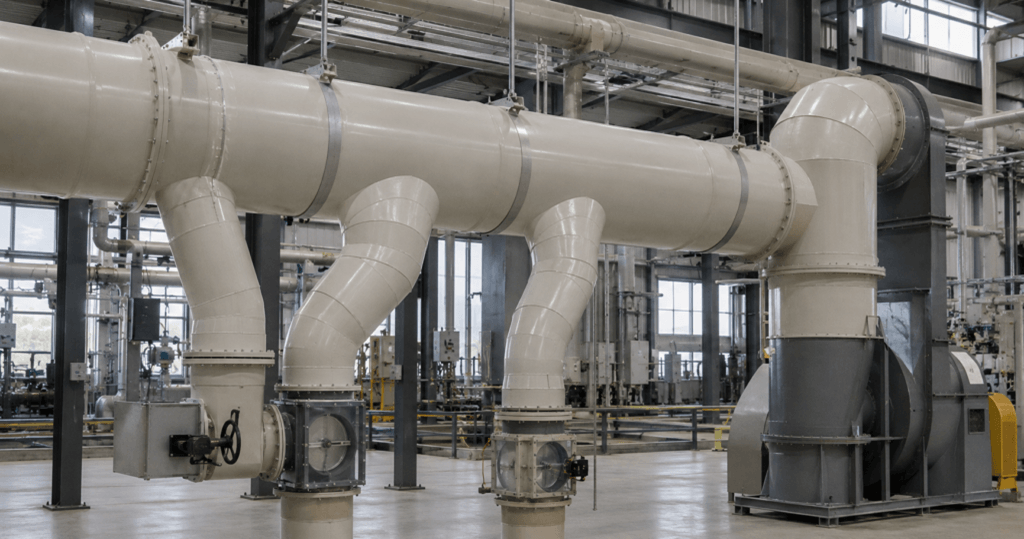
PDI manufactures matching PVC components including 90° elbows, reducers, wye branches, blast gates, saddle blast gates, and butterfly dampers. Those components should be selected as part of the pressure-loss model, not dropped into the layout after the main duct diameters are fixed. The next engineering resource in this cluster addresses duct elbow pressure loss in detail.
Branch Interaction Has to Be Reviewed by Operating StateScale
In a branched system, changing one path changes the resistance seen by the others. Closing a blast gate, modulating a damper, or taking a process tool offline can shift airflow and static pressure elsewhere in the network.
That is why balancing strategy belongs in the sizing discussion. If the system relies on manual gates, the design should define acceptable gate positions and operating combinations. If branches are modulated, the fan-control strategy and minimum system flow need to be considered. If all branches must maintain fixed capture performance over a wide operating range, the control approach may become as important as the nominal duct diameter
A well-sized system should not depend on excessive throttling to correct branch-to-branch differences created by poor geometry. Balancing devices are for commissioning and control; they are not a substitute for a coherent pressure-loss design.
Make-Up Air Is Part of the Exhaust Calculation
For large process-exhaust systems, building pressure can materially affect the delivered airflow. Insufficient make-up air increases building negative pressure and changes the pressure boundary the exhaust fan is working against. The result can be lower hood flow, difficult door operation, uncontrolled infiltration, or unstable balance between process areas.
The exhaust design basis should therefore include the make-up-air strategy and the building pressure relationship, especially where several large systems operate simultaneously. Treating replacement air as a separate comfort-HVAC issue can undermine an otherwise correct duct and fan calculation.
Confirm the Airflow Basis at Process Temperature
Industrial exhaust calculations may use actual CFM or standard CFM, and the distinction matters when gas temperature or density differs significantly from standard conditions. Velocity pressure measurements, fan performance, and mass flow can all be affected by the basis used.
For elevated-temperature exhaust, confirm whether the specified airflow is actual volume at duct conditions or a standardized volume corrected to reference conditions. Then carry the same basis consistently through velocity, pressure-loss, and fan calculations. The material check follows separately: PDI’s PVC duct temperature limits guide and PVC duct chemical resistance resource address whether PVC remains appropriate for the actual temperature and chemistry.
PVC Structural Limits Close the Loop
Aerodynamic sizing does not establish the structural adequacy of the duct. Once diameter and airflow are selected, the PVC construction still has to be reviewed for the maximum credible positive or negative static pressure, wall construction, unsupported span, reinforcement, fitting loads, support arrangement, and operating temperature.
This becomes more important as diameter increases. A larger duct selected to reduce velocity or pressure loss may move the project outside a standard extruded range or into a construction that requires project-specific fabrication. PDI’s guide to large-diameter PVC duct and custom fabrication covers that transition in more detail.
The same caution applies to pressure data: pressure-piping ratings should not be assigned to industrial ductwork. The duct construction and its positive/negative pressure capability need to be evaluated on duct-specific data and the actual fabricated system.
Commissioning Criteria Should Be Designed In
A sizing calculation is only useful if the installed system can be verified against it. Provide measurement locations and acceptance criteria while the duct is still being laid out—not after access is blocked by equipment and structure.
For critical branches, plan where airflow or velocity will be measured, where static-pressure readings can be taken, which gate or damper positions define the test condition, and what fan speed or operating mode applies. Straight, accessible traverse locations are more useful than trying to obtain representative readings immediately downstream of an elbow or branch.
Commissioning should confirm the parameters that matter to the design: source airflow, branch balance, fan operating condition, make-up-air operation, static pressure at reference points, and any evidence of leakage, deposition, condensate accumulation, or unexpected system resistance.
What Should Be in the PVC Duct Sizing Design Basis?
Before a PVC exhaust layout is released for fabrication, the design basis should identify: Balancing and commissioning measurement locations.
- Required airflow at each hood, enclosure, tool, or process connection.
- Coincident operating modes and diversity assumptions.
- Contaminant type and the engineering basis for design or minimum transport velocity.
- Candidate duct diameters and resulting actual velocities.
- The controlling pressure-loss path for each critical operating mode.
- Straight-duct friction plus losses through elbows, branches, reducers, gates, dampers, scrubbers, filters, stacks, and equipment connections.
- Fan operating point, speed/control strategy, and potential inlet or outlet system effect.
- Make-up-air and building-pressure assumptions.
- Actual-versus-standard airflow basis where temperature or density makes the distinction relevant.
- Normal and peak process temperature, chemistry, aerosols, and condensate.
- Maximum credible positive or negative static pressure.
- PVC wall construction, supports, reinforcement, and large-diameter fabrication requirements.
Diameter Is an Output of the System Design
The arithmetic that converts airflow and velocity into duct area is the easy part. The specification work is deciding which airflow belongs in each operating state, what velocity the process actually requires, which route governs fan duty, how fittings and controls alter the pressure profile, and whether the selected PVC construction remains suitable once pressure, temperature, chemistry, and support conditions are included.
That is why experienced industrial exhaust designers rarely defend a duct diameter with one velocity number. They defend it with a system model: source airflow, operating mode, contaminant behavior, pressure-loss path, fan performance, material envelope, and field verification all point to the same selection.
Need a PVC Exhaust Duct Configuration Reviewed?
Send PDI the branch airflow schedule, duct layout, process chemistry, normal and peak temperatures, fan information, operating modes, and expected pressure or vacuum conditions through the Request Information form. PDI can review the PVC/CPVC duct and fitting configuration and help identify where standard components or custom fabrication may be required.